Laser cutting can produce fine airborne particulate, metal oxides, hot particles, and sparks. What enters the collection system depends on the laser, table, assist gas, material, thickness, coatings or residues, production schedule, and how well the enclosure or downdraft zones capture the plume. Those variables affect filter loading, airflow, maintenance, worker exposure, and fire or explosion risk.
That is why a generic "dry dust" quote is not enough. Fine fume changes the filtration and capture problem, while the material and process determine whether the collected particulate is toxic, combustible, reactive, or incompatible with another stream. Paintbooth carries a broad line of dust collectors, but laser collection needs its own application review. The payoff is a shortlist built around the actual cut process, with the filter package, inlet arrangement, discharge method, and hazard controls evaluated as one system.
Fine fume changes the whole buying conversation
Coarse dust falls out of the air fairly fast. Laser fume doesn't. It hangs there longer, follows air currents, and reaches surfaces that may not look connected to the cutting area at all. That is a buying problem, not just a housekeeping problem, because the collector has to deal with what the process actually produces instead of what the shop happens to call it.
The practical effect shows up in four places:
A shop can ignore that pattern for a while, especially if the machine still cuts parts on schedule, but the cost shows up anyway. Fine fume doesn't stay politely above the cutting bed. It moves through the room, settles on ledges, and works into areas that take time to clean.
That is also why the dust-versus-mist distinction matters. Laser cutting usually belongs in a dry particulate and fume discussion, not a liquid overspray one. If a team is still sorting out equipment categories, the comparison on dust collectors vs. mist collectors helps clarify the line before a quote goes sideways.
Scenario one: a single enclosed fiber laser starts leaving haze around the machine
Imagine a fabrication shop with one enclosed fiber laser cutting most of the day. The owner does not see piles of debris around the table, so the first assumption is that the existing collector is close enough. Then the complaints start showing up in a more familiar way: a light film on nearby surfaces, more frequent cleanup, visible haze after long runs, and operators asking why the machine zone never seems fully clear.
That situation points to the real issue. The problem is not the lack of "dust collection" in the broad sense. The problem is that the contaminant is fine enough to behave like fume and smoke instead of falling out like heavier dust. A collector chosen for a different particle profile can miss the mark even if its cabinet size or motor spec looked respectable during the buy.
For that buyer, the right questions are concrete. What material is running through the laser most often? How many hours per shift? Where is the collector relative to the table? Is the duct route clean or awkward? How easy is it for maintenance to reach filters and service components? Once those answers are in the room, the collector discussion gets more honest fast.
Scenario two: a new laser table gets paired with the cheapest generic collector on the shortlist
The second common case shows up during expansion. A shop buys a new CO2 or fiber laser, then treats collection as an accessory line item and compares low bids from whatever dust equipment is already familiar. On paper, every option may sound acceptable because each one promises air movement and filter media. In practice, that is not enough.
Laser cutting introduces two issues that push this out of the generic category. First, the particulate is extremely fine. Second, the process can send sparks and hot material into the air stream. Those two facts affect the filtration package and the inlet protection strategy, which means a collector for ordinary shop dust may look cheaper at purchase and still cost more once downtime, filter changes, and cleanup show up.
This is usually where a laser-focused package starts making more sense than a generic cabinet. Not because every laser shop needs the same machine, and not because one model solves every application, but because the collector should be built around laser cutting from the start.
What buyers should define before comparing collectors
A good quote request for laser cutting dust collection does not start with horsepower. It starts with the table and the contaminant.
Bring these details into the discussion:
Photos help more than most buyers expect. A few shots of the table, the surrounding area, and the likely collector location can answer layout questions that a simple spec sheet misses.
It also helps to say what pain the shop is trying to stop. Some buyers want cleaner air around operators. Some want less residue on equipment. Some are replacing a collector that never felt right from the start. Those are different problems, even when the title on the quote says "laser dust collector."
Filtration and spark protection deserve close attention
Filter media has to match the particle characteristics and loading, but a rating on the filter does not prove that the table captures the plume or that worker exposure is controlled. The complete path matters: table enclosure or downdraft zones, duct airflow, leakage, filter condition, discharge, and the destination of cleaned air. Material-specific exposure concerns, including chromium-bearing alloys or coated stock, may require industrial hygiene review and air monitoring.
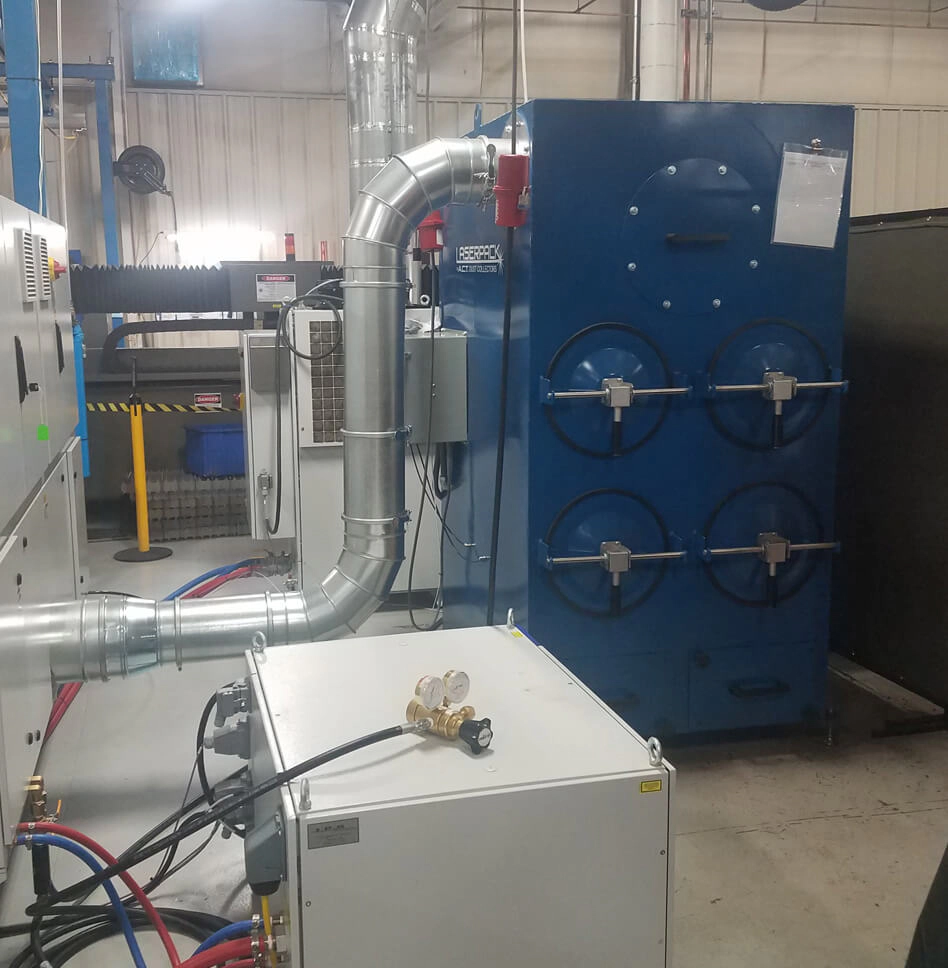
The Paintbooth LaserPack dust collector line is offered with Nano-Elite cartridge filters, flame-retardant filter options, a published MERV 15 rating, and an integrated cyclonic spark trap at the inlet. Those features address specific parts of filtration and inlet protection; they are not a complete fire or explosion design. Neither determines whether a particular dust is combustible or reactive, whether incompatible materials can mix, or what protection the duct and collector require.
That answer comes from a material and process hazard evaluation. It should address the alloys, coatings, dust test data when needed, ignition sources, mixed-material operation, collector location, dust discharge, and the prevention and protection measures required by the facility and authority having jurisdiction. Service access and footprint still matter, but they follow the contaminant and hazard decisions rather than replacing them.
A laser collector is also protecting the machine, not just the room
This point gets missed when buyers look only at air cleanup. Laser tables are expensive production equipment. Fine particulate that escapes capture does not disappear. It settles on nearby surfaces, enters maintenance areas, and adds contamination around assets the shop depends on every day.
That makes collection part of machine protection. Better capture can reduce the film that builds up around the table, cut down on repeated wipe-down work, and help the area stay more stable during long runs. The savings are not always dramatic in a single afternoon, but they become obvious over months of production when the shop is no longer fighting the same residue in the same places.
For maintenance teams, this is usually where the argument becomes easy. If the current setup leaves cleanup behind every shift, the collector is not finished doing its job just because it runs.
Questions worth asking before you buy
Before choosing a collector, push past the generic brochure language and ask a few direct questions.
Those questions tend to separate real application review from box-comparison selling.
The right next step
If your shop is planning a new laser install, replacing a collector that never handled the fume well, or trying to stop haze and residue around an existing table, start with the process details rather than a generic equipment request. Paintbooth can review the laser type, table layout, material mix, production schedule, and collector location to help narrow the right path.
Use the quote request form and include photos of the table, available collector space, duct path, and the issue you are trying to fix. That gives the team enough context to sort whether a LaserPack configuration or another collection approach makes sense for your shop.