Cartridge dust collectors are common in industrial finishing, but "dry particulate" is only the first decision gate. The material being worked, the way the process changes it, particle size and loading, moisture, temperature, toxicity, combustibility, and possible ignition sources can all change the filter media, collector configuration, discharge method, or collection technology. A sanding bench and a laser table may both create dry airborne material without presenting the same filtration or fire problem.
That is why a useful quote starts with the process and material rather than a cabinet size. Paintbooth's dust collector lineup covers a wide range of industrial collection equipment, and its cartridge dust collector page includes metalworking, blasting, laser, and weld-related applications. The payoff for the buyer is a defensible shortlist: where cartridge collection fits, what application details control the choice, and when another approach needs review.
The first filter is the material itself
The first gate is the material that becomes airborne and the process that creates it. A dry stream can put cartridge filtration into consideration; it does not establish suitability by itself. Sanding dust, grinding fines, powder residue, hot cutting particulate, and blast debris can differ in size, loading, abrasiveness, temperature, moisture, toxicity, and fire or explosion behavior.
Start with the base material, coatings or residues on the part, process consumables, and any safety data available. If the dust may be combustible or reactive, the equipment decision also needs the facility's hazard evaluation and any material testing required to characterize that risk. Mixed process streams deserve the same care because materials that are manageable separately may create a different hazard when collected together.
Wet overspray, sticky residue, and oil mist begin in a different equipment category; Paintbooth's dust-versus-mist guide helps draw that line. Toxic particulate also changes the review because capture, filtration, discharge, housekeeping, and any return-air decision must support the facility's exposure-control plan. The machine name comes after those facts, not before them.
Scenario one: one dusty station, one clear source
Suppose a finishing shop has a single sanding and deburring station next to the paint-prep area. Operators run the station most of the day, the dust settles on nearby carts, and the cleanup burden keeps creeping into the rest of the department. That is the kind of problem where a compact cartridge collector often fits well.
In a case like that, the source is localized. The process is known. The collector can be selected around a fixed capture point, a short duct run, and a manageable service routine. The shop does not need a plant-wide system; it needs a collector that can stay close to the work, pull dry particulate away from the operator zone, and remain easy to service.
This is where compact cartridge units earn their keep. Paintbooth's cartridge line includes smaller units used around localized metalworking, blasting, laser-table support, and similar dry-dust applications. The value for a buyer is not a generic promise of versatility. It's the ability to solve one defined mess without paying for a larger central network the shop does not need yet.
If your situation looks like this, gather the facts that actually shape the quote: what part gets worked on, what tool creates the dust, how long the station runs, whether the dust load spikes on certain jobs, and where the collector could sit without creating a maintenance headache. A concise process description often does more for quote accuracy than a page of broad requirements.
Scenario two: several dirty points feeding one facility
Now change the picture. A fabrication and finishing operation has multiple work points: two grinding stations, a cut-off area, several weld cells, and a prep zone ahead of coating. Dust and fume are not coming from one bench; they are scattered through the department. Housekeeping has become inconsistent, and the finishing team is tired of contaminants migrating into cleaner areas.
That is usually a larger collector conversation. Cartridge filtration may still fit the job, but the buyer has moved from point-of-use collection to a broader system question. Larger cartridge units are often used across multiple areas in a facility, including several process points tied into one collection strategy. At that scale, the cabinet matters less than the capture plan, duct routing, access for service, and whether all pickup points will run at once.
This is where buyers need to slow down and resist two bad habits. The first is under-scoping the project by quoting only the dirtiest station and hoping the rest of the plant will somehow improve. The second is over-scoping it with vague future growth and ending up with an expensive system built around guesses. A better approach is to map the current sources, note which ones run at the same time, and identify the stations that truly need to be part of the same collector strategy.
For multi-point collection, layout discipline matters. A cartridge collector may still be right, but the job now depends on how the air gets from each source to the unit, how the collector will be emptied and serviced, and whether the chosen location helps or hinders the department that has to live with it.
Where cartridge collectors usually fit best
Cartridge collectors tend to fit industrial finishing support work in four common situations.
One is sanding, grinding, or deburring ahead of coating, where dry particulate can contaminate parts and nearby work surfaces. Another is blast-related support work or other dry prep operations that need dust capture but are not paint booth exhaust systems. They also show up around fabrication areas that feed the finishing line, especially where weld smoke, cut particulate, or dry residue would otherwise drift toward cleaner operations. And they can support specialized dry applications such as certain laser-table or powder-handling environments when the contaminant profile matches the equipment.
The connecting thread is plain: the collector is handling dry airborne material from a known source. It is not standing in for a spray booth exhaust package, and it is not a cure-all for undefined dirt in a building.
Maintenance should influence the purchase early
Buyers often spend most of the conversation on airflow and very little on upkeep. That's backwards. If the collector will be hard to service, performance problems tend to show up later as delayed filter changes, messy access, or workarounds the maintenance team never wanted.
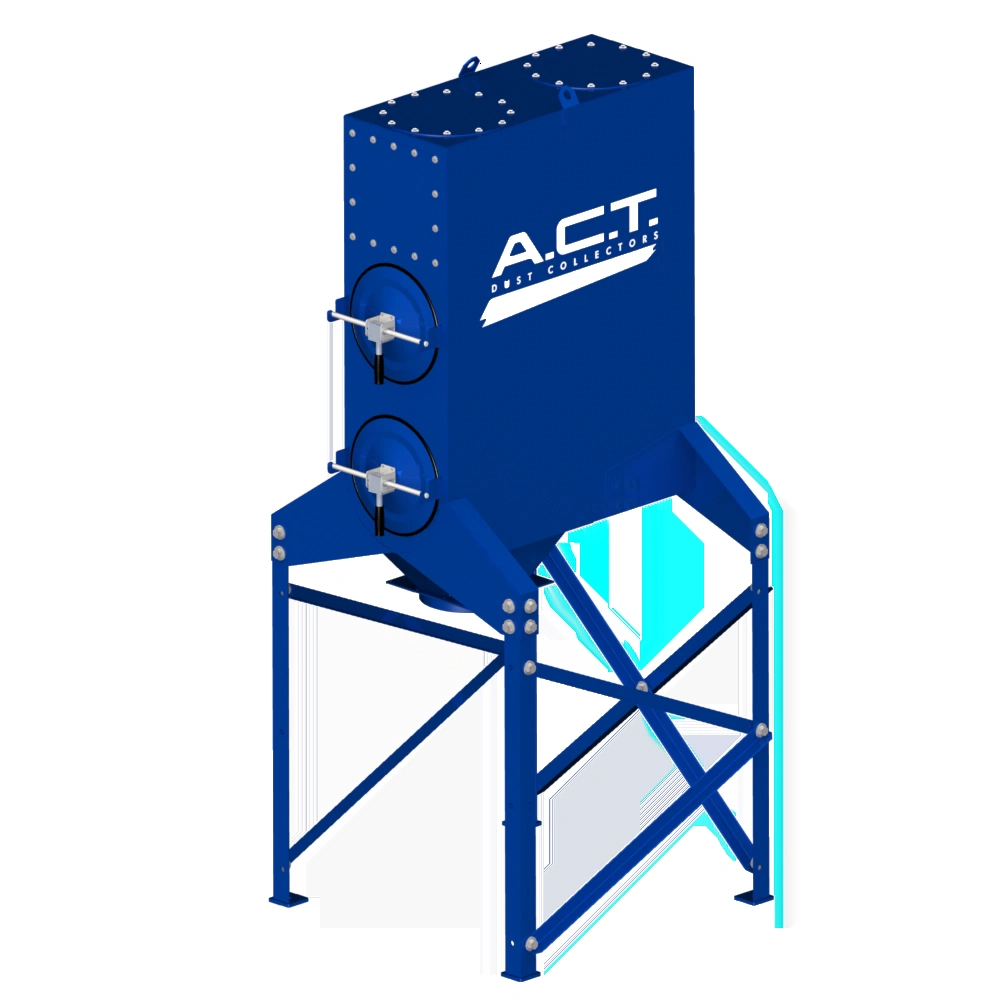
The cartridge product material repeatedly points to downward airflow, pulse-style filter cleaning, quick-access filter doors, and standard-sized replacement filters. Those are useful details because they affect ownership cost and downtime. They also affect whether the collector will still be getting proper service a year after startup, when production pressure is higher and the new-equipment attention has worn off.
Ask direct questions before the quote turns into a purchase order. How many filters are in the proposed unit? Where will a technician stand to change them? Does the collector location leave enough clearance for doors and access panels? Is the dust drawer or hopper easy to reach, or did the layout push it into a cramped corner because floor space looked better on paper than it does in the actual plant?
A cartridge collector can be the right technical fit and still become the wrong practical fit if nobody plans for maintenance access.
Published ranges are helpful, but they don't size the system
Paintbooth's cartridge category material describes standard units from smaller horsepower and airflow ranges into much larger industrial capacities. That is useful for one reason: it tells buyers the product family covers both compact and facility-scale applications.
It does not tell you what your shop needs.
The right collector depends on how capture will happen, how many pickup points are active, what the material load looks like, how the duct runs will be laid out, and what the operating schedule really is. A buyer should treat published range examples as proof that the category spans small and large jobs, then move quickly into project specifics.
Lead-time language deserves the same caution. If a source mentions fast availability on many standard units, treat that as something to confirm during quoting, especially if the project needs accessories, a custom arrangement, or a layout that will affect installation.
Signs that another collection approach may be needed
A cartridge collector is not the default answer every time a process makes dust. Wet or sticky material, oil-laden air, elevated temperature, very heavy or abrasive loading, toxic contaminants, and difficult discharge requirements may point to different media, pretreatment, collector construction, or another collection method. Uncontrolled material handling or poor separation between dirty prep work and clean finishing work may also require process changes beyond the collector.
Unknown combustibility or reactivity is a reason to pause equipment selection until the material is characterized. Sparks, hot particulate, combustible dust, or incompatible materials in a shared system require a fire and explosion review based on the actual process. A flame-retardant filter or an inlet device may be one part of a design, but neither answers the full hazard question on its own.
What a buyer should have ready before asking for a quote
The most useful quote requests are specific. Not polished, just specific.
Bring the process type; base materials, coatings, and consumables; available safety data; number of stations; run time; and which collection points operate together. Describe whether the material is dry, damp, sticky, hot, abrasive, toxic, combustible, or potentially reactive, and include particle-size, dust-loading, or explosibility test data when the facility has it. Note nearby spark-producing work, the proposed dust-discharge method, and whether filtered air is being considered for return to the building.
Add the preferred equipment location, photos, and dimensions that affect duct routing, ceiling height, traffic lanes, electrical service, and filter access. If an older collector is being replaced, explain what is failing now: short filter life, poor capture, awkward service, escaping dust, or production growth. For material-specific exposure or fire questions, include the industrial hygiene or fire-protection criteria the finished system must satisfy rather than expecting a generic collector quote to define them.
That gives Paintbooth something real to work from. It also makes the answer sharper: a small collector near one prep station, a larger cartridge system for several work zones, or a recommendation to review a different collection category before moving ahead.
A practical buying read
Cartridge dust collectors fit industrial finishing work when the contaminant has been characterized, cartridge media and construction suit that material, and the capture, discharge, exposure-control, and fire-protection plans agree with the application. They can serve localized prep stations or larger multi-point systems, but dry particulate alone is not the deciding fact.
If you're sorting through that choice now, start with the process description instead of the model number. Then use Paintbooth's cartridge dust collector category to narrow the options, and send the real application details through the quote request form. A few photos, station count, material notes, and layout constraints will usually move the conversation further than a broad request for "a dust collector for finishing."