

The true operating cost of an industrial sandblasting booth is rarely captured by a simple hourly rate. Total operating expense depends on compressed air generation, abrasive media breakdown, and direct labor, measured over compatible operating periods. Budgeting based solely on an eight-hour shift schedule can distort costs by failing to separate trigger time from booth occupancy time, masking, and parts handling.
Building an accurate operational budget requires breaking down each physical input, accounting for abrasive reclaim efficiency, and budgeting for the inevitable wear on filtration and booth components.
Choose a Useful Cost Unit: Define the Production Unit and Operating Hours
A blast booth budget built around facility shift hours rather than nozzle trigger hours will distort your cost projections. Measure how much of each shift the operator actually blasts. Other time is consumed by staging parts, rigging, masking critical surfaces, post-blast blow-down, and sweeping abrasive.
To build a reliable cost model, establish a metric that reflects your production reality:
- Cost per Trigger Hour: The baseline engineering metric. It measures the precise cost of running the blast nozzle continuously for 60 minutes.
- Cost per Square Foot: The standard for structural steel, plate, or tank fabrication. It normalizes costs against surface cleanliness specifications (such as an SSPC-SP 10 near-white blast versus an SSPC-SP 7 brush-off blast).
- Cost per Finished Part or Assembly: The preferred metric for batch manufacturing and repetitive job shop components, factoring in masking and handling complexity.
Your choice of baseline unit directly influences how you evaluate capital equipment. When comparing different sandblasting booth options, a design that shortens material handling—such as an overhead monorail or an automated floor reclaim system—reduces non-blasting labor. That efficiency lowers your total operating cost per completed part, even if the hourly cost to generate compressed air remains identical.
Measure Air, Abrasive, and Labor Inputs
The direct operational expense of blasting breaks down into three core categories: energy for compressed air, media consumption, and labor.
- Period Operating Cost = Air Energy Cost + Net Media Cost + Direct Labor Cost + Maintenance & Waste Costs
- Cost per Accepted Part = Period Operating Cost / Accepted Parts in That Period
- Air Energy Cost = [(Loaded kW × Loaded Hours) + (Standby kW × Standby Hours)] × Electricity Rate ($/kWh)
- Net Media Cost = Initial Charge Cost Allocated to Period + (Make-Up Media Used in Period (lb) × Delivered Cost ($/lb))
- Direct Labor Cost = Sum of Each Worker’s Burdened Hourly Rate ($/hour) × Their Paid Hours in Period
1. Compressed Air Demand and Electrical Costs
Compressed air is usually the single largest utility cost in abrasive blasting. Air consumption is governed by nozzle orifice size and operating blast pressure.
Reference data published by equipment manufacturers such as Clemco illustrates that air volume requirements scale rapidly with nozzle wear and operating pressure. A larger nozzle orifice—including one enlarged by wear—requires more compressed air at the same operating pressure. Use the manufacturer’s chart for the selected nozzle and pressure to estimate the change.
To convert this physical requirement into a facility-specific operating cost:
- Check your compressor's specific power output: Use measured input power and delivered air at your actual operating pressure, or the compressor manufacturer’s performance data.
- Factor in compressor duty cycle and unload states: Unloaded or idling compressors can still consume power; the amount depends on their control arrangement.
- Apply your utility tariff: Multiply total kilowatt-hours (blasting load plus idle time) by your local electric utility rate, then account separately for any tariff demand charges.
If your facility operates at lower pressures or uses non-standard nozzle geometries, consult the compressor’s specific performance curves and pressure drop ratings across your dryer and piping package rather than relying on generic rules of thumb.
2. Abrasive Media Consumption and Attrition
Media costs depend in part on whether your booth runs an expendable (single-use) abrasive or a recyclable media system.
Expendable abrasive consumption depends on nozzle size, metering valve adjustment, media properties, and the work; measure your actual usage per trigger hour. Consumption tables published by manufacturers indicate general delivery volumes based on assumed media weights (check the chart’s stated density). If you run expendable media, your period material cost is straightforward: delivered cost per ton multiplied by actual tons consumed during the period.
Recyclable abrasives (such as steel shot, steel grit, or aluminum oxide) add recovery equipment and an initial media charge, but can reduce replacement-media costs when the application supports reuse. Here, calculating expenses requires understanding how blast media recycling works within a mechanical recovery circuit. In systems utilizing mechanical recovery—such as a bucket elevator feeding an air-wash separator (seen in designs like the Clemco AWAC)—the spent media is swept or augured into an elevator boot, lifted into the cleaner. In the AWAC example, a rotating screen rejects oversized debris, and an air wash separates lighter fines from reusable abrasive. Clean, reusable media drops back into the storage hopper above the blast machine.
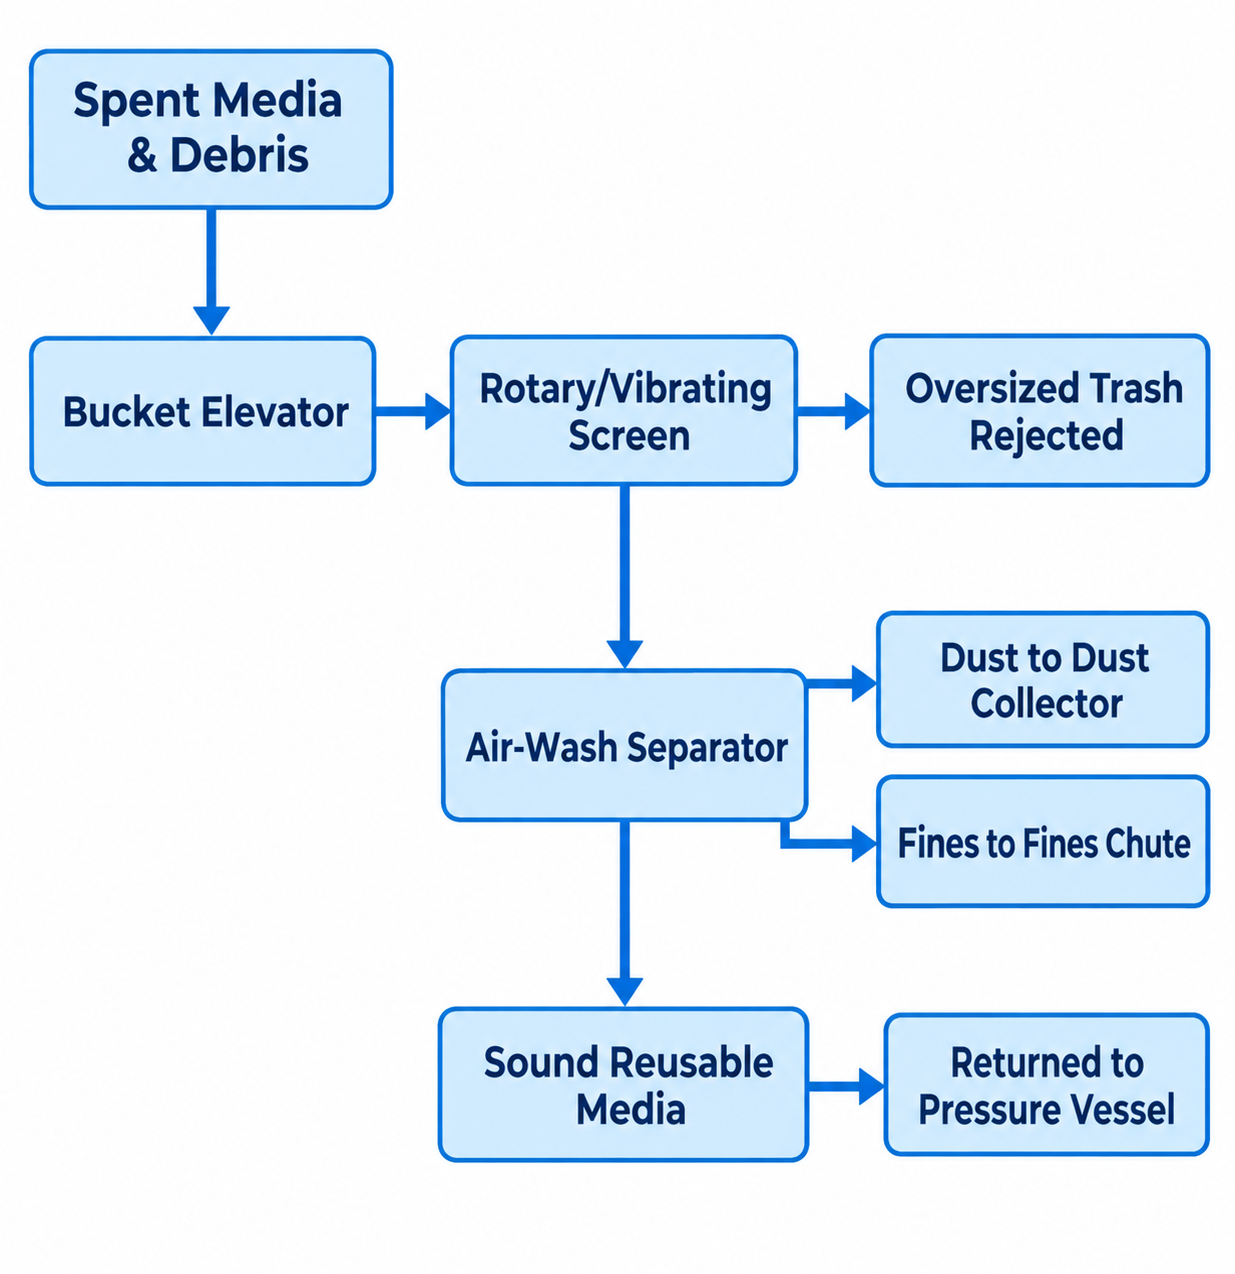
Diagram description
- Spent Media & Debris
- Bucket Elevator
- Rotary/Vibrating Screen
- Oversized Trash Rejected
- Air-Wash Separator
- Dust to Dust Collector
- Fines to Fines Chute
- Sound Reusable Media
- Returned to Pressure Vessel
- Spent Media & Debris → Bucket Elevator
- Bucket Elevator → Rotary/Vibrating Screen
- Rotary/Vibrating Screen → Oversized Trash Rejected
- Rotary/Vibrating Screen → Air-Wash Separator
- Air-Wash Separator → Dust to Dust Collector
- Air-Wash Separator → Fines to Fines Chute
- Air-Wash Separator → Sound Reusable Media
- Sound Reusable Media → Returned to Pressure Vessel
- Spent Media & Debris → Bucket Elevator → Rotary/Vibrating Screen.
- Screen branches right to Oversized Trash Rejected and down to Air-Wash Separator.
- Separator branches right to Dust to Dust Collector, right separately to Fines to Fines Chute, and down to Sound Reusable Media.
- Sound Reusable Media → Returned to Pressure Vessel.
However, media recycling is not perpetual:
- Attrition Rates: Media breaks down through repeated impacts; usable life varies with abrasive type, blast conditions, and the required surface result. You must budget for regular additions of "make-up" media to keep the operational mix balanced.
- Contamination Limits: Mechanical separation only sorts particles by physical size and aerodynamic density. It cannot wash out soluble salts, oils, or grease. If your raw parts carry heavy cutting fluids, recycling abrasive across them transfers those hydrocarbons into the entire media batch, requiring premature media disposal regardless of particle size.
3. Direct and Support Labor
Abrasive blasting is physically demanding, high-risk work that demands qualified labor. When calculating labor cost, include:
- The primary blast operator’s burdened wage (base rate plus benefits, workers' comp, and mandatory PPE allowances).
- Pot tender or material handling labor required to stage parts, load the pressure vessel (if non-automated), manage blast hoses, and supervise the compressor.
- Post-blast cleanup labor, including blow-off, masking removal, and sweeping media from deep pockets within complex fabrications.
Include Maintenance, Filters, and Waste Handling
Operating budgets routinely fail by omitting the ongoing wear on the booth itself. Abrasive dust attacks every mechanical component inside the blast envelope.
Wear Components and Blast Consumables
Budget for these high-wear items based on trigger hours:
- Blast Nozzles: Tungsten carbide nozzles offer lower initial cost but wear quickly when using aggressive media like aluminum oxide or silicon carbide. Compare liner purchase price and wear life for your abrasive; longer orifice life can limit growth in air demand.
- Hoses, Gaskets, and Couplings: Blast hose interiors erode, particularly on the outer radius of bends. Whip hoses and coupling gaskets require inspection and changeouts under the equipment manufacturer’s maintenance instructions to prevent blowouts.
- Operator Safety Equipment: Positive-pressure blast helmets require ongoing inspection and replacement of protective lenses, breathing-air system consumables, and cape attachments as specified by their manufacturers.
- Internal Wall Curtains: Budget for the wall protection specified for your blast room, which may include heavy hanging rubber or polyurethane curtains. Direct blast impingement or abrasive rebound will eventually cut through these curtains, exposing the booth's steel structure to wall thinning and perforation.
Ventilation and Dust Collector Maintenance
The ventilation system must maintain the airflow specified for the enclosure, media, and process to maintain operator visibility and capture airborne particulates.
- Cartridge or Bag Replacement: Filter life depends on your air-to-cloth ratio, pulse-jet cleaning efficiency, and the hygroscopic nature of the dust. Budget for full filter element replacement based on the manufacturer’s condition and differential-pressure criteria.
- Pulse-Jet Air Consumption: Reverse-pulse dust collectors consume dry, clean compressed air during cleaning pulses to clean their filters during operation. This air draw must be added to your overall compressor operating load.
Spent Media Disposal and Environmental Testing
Disposing of spent abrasive and collected dust is governed by the chemical composition of the substrate and coatings you remove:
- Toxicity Characteristic Leaching Procedure (TCLP): If you blast mill scale on clean carbon steel, your spent media and dust cake may qualify as non-hazardous industrial waste. If you strip structural steel painted with lead-based primers, marine anti-fouling coatings, or chromate conversion coatings, your waste may be classified as hazardous.
- Disposal Tonnage Fees: Waste classification affects disposal quotes, hauling, documentation, and storage requirements; confirm these costs for your waste stream. Secure an analytical profile and pricing from a licensed industrial waste handler before finalizing your operational budget.
Compare Estimates at Realistic Utilization
A static spreadsheet model based on 100% capacity will provide a false sense of security. Variable operating costs behave differently depending on booth utilization, process rework, and the speed of media recovery. The following table shows planning tendencies to test against your actual operation.
| Operating Parameter | Low-Volume Run | Steady Production | Multi-Shift Heavy Production |
|---|---|---|---|
| Potential Cost Emphasis | Labor (staging, handling, waiting) & Standby Power | Balanced: Labor, Energy, and Media | Energy, Media Attrition, and Component Wear |
| Recovery Options to Evaluate | Expendable or Slow-Payback Recyclable | Recyclable (Mechanical Floor or Sweep-In) | Fully Automated Recyclable Reclaim |
| Filter & Wear Costs | Low frequency, tied to calendar time | Moderate frequency, predictable schedule | High frequency, often driven by usage and condition |
| Fixed Cost Impact | High overhead cost per processed part | Normalized overhead distribution | Lowest overhead allocation per processed part |
The Cost Penalties of Rework
Surface preparation standards allow narrow margins for error. If an operator applies an inconsistent blast pattern, leaves oil streaks, or creates an improper surface anchor profile (too shallow for coating adhesion or too deep, causing pinhead rust), the part may need additional preparation or rework.
Rework adds labor, air energy, and media cost while consuming booth capacity; its effect depends on how much processing must be repeated. Base a scrap/rework allowance on your measured history or documented project assumptions.
Reclaim Floor Efficiency
The speed of abrasive recovery dictates how quickly the booth can process subsequent batches:
- Partial Reclaim / Sweep-in Pits: Lower initial equipment cost, but significant manual labor is required to shovel or push media into the recovery pit. The booth sits idle while blasters sweep, running down utilization rates.
- Full Reclaim Floors (Pneumatic or Mechanical): The entire floor automatically recovers, cleans, and returns abrasive to the blast generator continuously. This can reduce recovery delays, but mechanical maintenance (screws, belts, floor grates) must be added to your ongoing ledger.
When you are ready to reach out to an equipment manufacturer to request a blast booth quote, bring your specific operational data rather than asking for broad industry averages. Arriving with a defined part profile, your desired blast standard (e.g., SSPC-SP 10), your anticipated trigger hours per day, and your local electricity rate enables suppliers to engineer an airflow, reclaim, and compressor package sized to meet your actual per-part budget targets.
Translating Cost Models into an Equipment Inquiry
To verify your operating cost model against real-world equipment capabilities, collect the following mechanical and facility specifications from your team before engaging suppliers:
- Air System Capacity: What is the actual delivered CFM of your current compressor plant at the intended operating pressure, and what is your documented cost per kWh during peak operating shifts?
- Substrate and Coating Profile: What specific coatings, oxides, or contaminations will you remove, and what waste characterization and disposal requirements apply?
- Cleanliness and Anchor Pattern: What specific surface profile depth (mils) and visual cleanliness specification (SSPC/NACE/ISO) does your downstream coating specification mandate?
- Target Part Geometry: What are the maximum dimensions, weights, and daily throughput counts of the parts entering the blast enclosure?
- Floor Reclaim Expectation: Does your production timeline require an automatic full-recovery floor for continuous blasting, or can your workflow accommodate manual push-in or partial reclaim designs?