

A drop in booth performance or a sudden wave of surface defects rarely points to a single obvious culprit. Adjusting burner controls on a hunch or blaming ceiling media for every crater on a clearcoat wastes billable hours and risks masking the true fault.
Effective troubleshooting relies on disciplined triage: document the active state, separate cabin ventilation issues from coating chemistry, and capture clear evidence before altering equipment settings or paging an outside technician.
Log Context and Operating Conditions Before Adjusting Equipment
Equipment settings should remain untouched until the exact operating conditions surrounding an anomaly are documented. Modern spray cabins rely on interlocked mechanical systems where an unexpected shutdown or airflow drop is frequently a protective response rather than an isolated component failure.
INITIAL TRIAGE CHECKLIST
- 1. Operational Mode
- Spray, Flash, Cure/Bake, or Exhaust Purge
- 2. Fault Category
- Airflow interlock, burner, limit switch
- 3. Substrate & Chemistry
- Substrate material, clear/base/primer lot
- 4. Spatial Pattern
- Targeted panel, entire rack, whole cabin
- 5. Recent Facility Changes
- Filter swaps, airline service, weather
When an alarm triggers or a cycle interrupts, record the baseline operational state:
- Current operating cycle: Identify whether the fault occurred during Spray, Flash-off, Cure/Bake, or Exhaust Purge. Record displayed temperatures and timer values, distinguishing setpoints from measured sensor readings; a local sensor reading does not establish conditions throughout the cabin.
- Active fault annunciations: Note specific control codes. A burner lockout, high-limit trip, or exhaust interlock requires consulting equipment-specific control guidance rather than cycling the power to force an override. Never bypass safety interlocks to complete a job.
- Coating and substrate variables: Record the paint line, activator selection, reducer speed, and substrate material. Note whether the issue affected an entire production batch or a single isolated component.
- Physical distribution: Determine if the symptom is cabin-wide, confined to one bay corner, or tracking with an individual operator or fluid line.
- Timeline and maintenance history: Verify whether the anomaly began abruptly mid-cycle, developed gradually across several shifts, or followed an intake filter change, compressed air compressor servicing, or severe weather shift.
Separate Equipment Malfunctions from Coating Chemistry
Surface anomalies often look like mechanical booth failures when they actually originate in chemistry, fluid preparation, or substrate handling. Conversely, operators sometimes blame product batches for dry spray or solvent boil caused by uncalibrated airflow or drifting bake temperatures.
Dividing symptoms into two operational groups prevents misdirected labor:
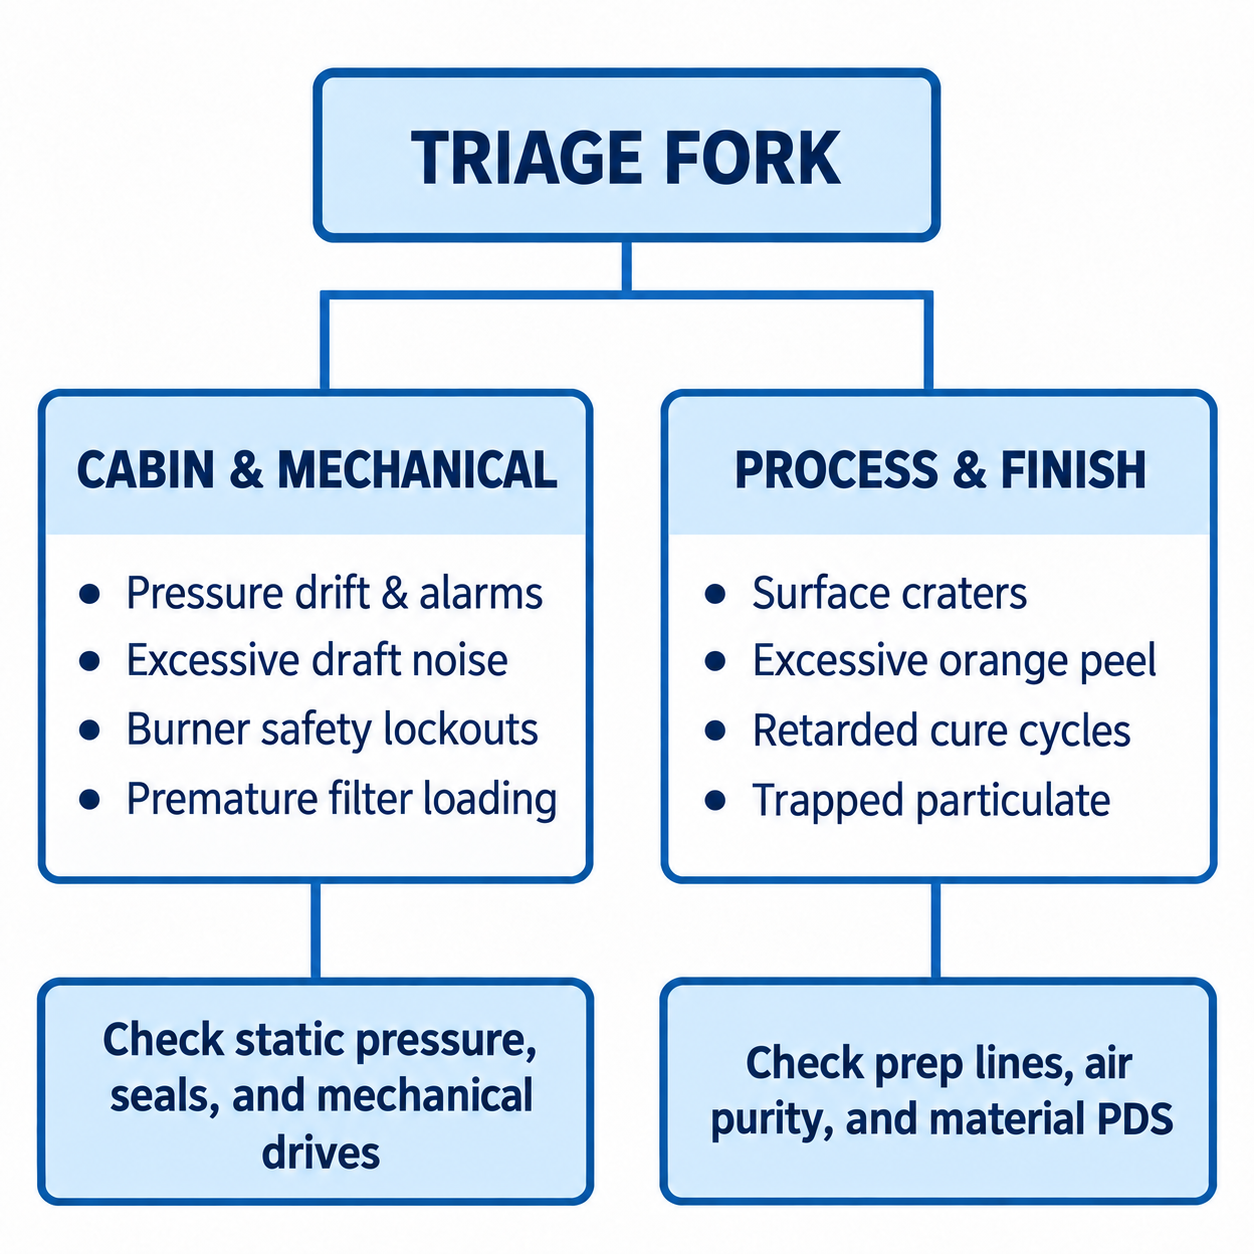
Diagram description
- TRIAGE FORK
- CABIN & MECHANICAL
- Pressure drift & alarms
- Excessive draft noise
- Burner safety lockouts
- Premature filter loading
- Pressure drift & alarms
- Excessive draft noise
- Burner safety lockouts
- Premature filter loading
- Check static pressure, seals, and mechanical drives
- PROCESS & FINISH
- Surface craters
- Excessive orange peel
- Retarded cure cycles
- Trapped particulate
- Surface craters
- Excessive orange peel
- Retarded cure cycles
- Trapped particulate
- Check prep lines, air purity, and material PDS
- TRIAGE FORK → CABIN & MECHANICAL
- CABIN & MECHANICAL → Check static pressure, seals, and mechanical drives
- TRIAGE FORK → PROCESS & FINISH
- PROCESS & FINISH → Check prep lines, air purity, and material PDS
- TRIAGE FORK connects via undirected fork lines to CABIN & MECHANICAL and PROCESS & FINISH
- Mechanical contains its four symptom bullets then connected bottom check label
- Process contains its four symptom bullets then connected bottom check label
- No cross-column links
Ventilation, Pressure, and Cabin Hardware
Mechanical faults typically reveal themselves through air pressure shifts, audible motor strain, or cycle interruptions:
- Airflow differential switches tripping during mode changes.
- High positive cabin pressure forcing overspray out around access door perimeter seals.
- Excessive negative pressure making personnel doors difficult to unlatch.
- Unusual vibration, belt squeal, or housing resonance within exhaust ducting.
These indicators support investigation of physical air handling, including filters, drives, dampers and blower condition; they do not identify a failed component on their own.
Texture, Contamination, and Drying Performance
When equipment runs without alarms yet finishes display visible defects, evaluate application variables alongside environmental conditions:
- Surface craters and dewetting: Cratered depressions do not confirm contaminated ceiling filters. Oil blow-by from shop compressors, silicones from nearby panel bonding, poor degreasing methods, or contaminated air hoses frequently create identical defects. Compare shop floor observations against established fisheye defect guidance before condemning booth filtration.
- Irregular surface texture: Pronounced ripples or dry spray are frequently driven by gun distance, incorrect fluid nozzle sizes, or solvent flash timing that conflicts with cabin air velocity. Operators should review verified orange peel guidance and material viscosity before suspecting ventilation issues.
- Extended cure times: Soft film or persistent tackiness often stems from off-ratio hardeners, excessive wet film thickness, or applying fast reducers in high-load situations. Cross-reference actual paint properties with slow-drying guidance and the coating manufacturer’s technical data sheet (PDS) before concluding the heating plant is failing.
If the symptom appears exclusively on the painted product while equipment observations remain normal, include paint finish diagnosis in the initial investigation. Normal displays alone do not rule out booth environmental conditions.
Narrow Plausible Causes with Targeted Observations
Moving from a symptom to a root cause requires targeted, non-invasive observations. Isolate one variable at a time using this observation matrix:
| Observed Symptom | Primary Data Point | Potential Variables | Next Verification Step |
|---|---|---|---|
| Abrupt jump in differential pressure | Magnehelic / digital pressure gauge | Face-loading, misaligned media, blown track | Review filter inspection records; inspect exhaust bank for frame gaps or roll blow-by. |
| Recurring dirt in one zone | Defect map across panels | Door seal tear, dead air pocket, linty clothing | Record visible door-seal damage and the affected location; leave airflow testing to a qualified, site-authorized measurement plan. |
| Finish fault limited to one coating layer | Primer vs. base vs. clear evaluation | Mix ratio, flash window, gun supply line | Check the product PDS; verify flash timer accuracy and dedicated airline filtration. |
| Dimming or yellowed illumination | Visual inspection of light bays | Overspray crust, failing ballast, old tubes | Clean exterior glass shields; check relamping schedules per manufacturer maintenance instructions. |
| Uneven cure across the vehicle | Part surface temperature readings | Heat stratification, duct blockage, airflow shadow | Record the affected part locations and start temperature imbalance troubleshooting using authorized measurement methods. |
Practical Observation Scenarios
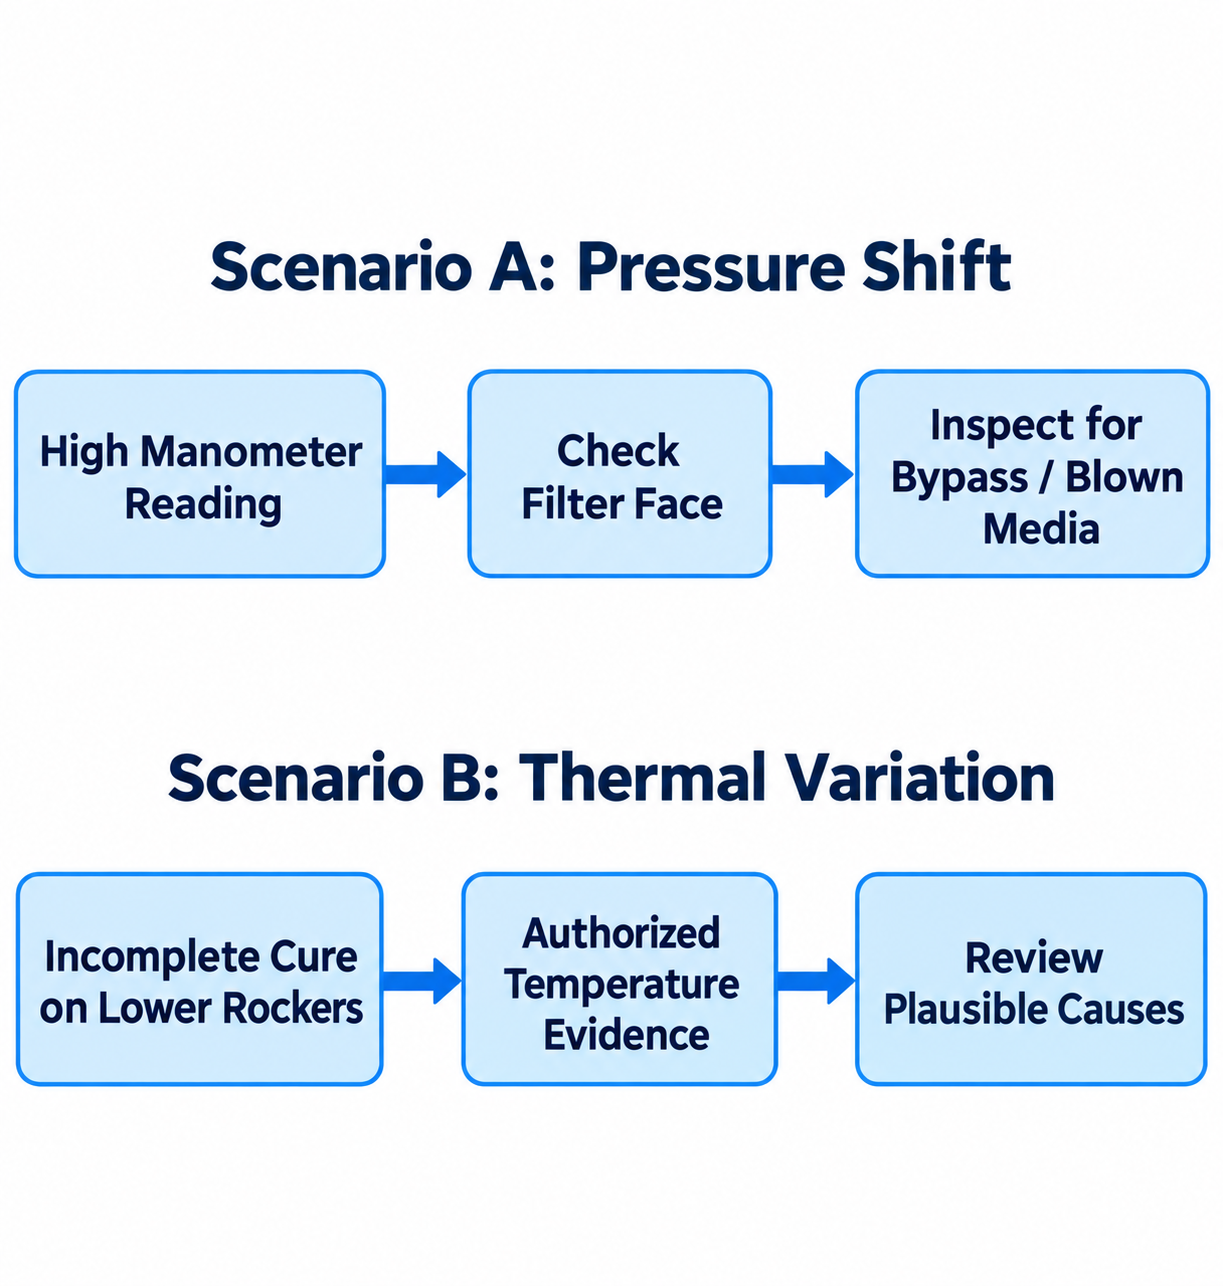
Diagram description
- Scenario A: Pressure Shift
- High Manometer Reading
- Check Filter Face
- Inspect for Bypass / Blown Media
- Scenario B: Thermal Variation
- Incomplete Cure on Lower Rockers
- Authorized Temperature Evidence
- Review Plausible Causes
- High Manometer Reading → Check Filter Face
- Check Filter Face → Inspect for Bypass / Blown Media
- Incomplete Cure on Lower Rockers → Authorized Temperature Evidence
- Authorized Temperature Evidence → Review Plausible Causes
- Two independent flows: Scenario A: Pressure Shift: High Manometer Reading → Check Filter Face → Inspect for Bypass / Blown Media.
- Scenario B: Thermal Variation: Incomplete Cure on Lower Rockers → Authorized Temperature Evidence → Review Plausible Causes.
1. Abrupt Static Pressure Reading Shifts
When a differential pressure gauge spikes unexpectedly, do not assume exhaust filters are exhausted from overspray loading alone. Arrange inspection of media seating under the equipment’s authorized maintenance and isolation procedure.
A roll pulled away from its retaining track lets air bypass the media, dropping resistance, while a misaligned pre-filter can load unevenly and elevate resistance rapidly. Verify findings against recorded historical baseline pressures.
2. Localized Finish Contamination
If particulate lands repeatedly on the same panel across consecutive runs, record that spatial pattern and investigate local sources alongside booth-wide conditions.
Examine the door seals adjacent to that corner for tears, inspect door thresholds for tracked-in sanding dust, and observe whether operators stage prep carts directly upwind of that zone.
3. Single-Stage Finish Defects
When a primer surfacer sands cleanly and basecoat lays flat, but clearcoat exhibits micro-pinholing or solvent pops, compare layer-specific application variables alongside ventilation and temperature observations.
Possible variables include flash timing between coats, spray viscosity and the coating’s drying conditions. Always confirm the actual material requirements on the PDS.
4. Lighting Degradation
Loss of illumination alters an operator's fluid overlap and travel speed, producing dry spray mistaken for poor downdraft performance.
Inspect protective glass panels for overspray crusting before testing ballasts or replacing tubes. Use only the manufacturer-approved cleaning and lens-protection methods for the installed assembly.
5. Localized Under-Cured Paint
If lower body rockers remain tacky while roof sections cure hard, investigate thermal variation alongside coating thickness, mixing and application history.
Use a qualified, site-authorized measurement plan to compare substrate temperatures at the affected locations. If readings differ from the coating’s specified conditions, provide the evidence to qualified service personnel without treating it as proof of a damper or burner fault.
Build an Actionable Service Record to Speed Up Repairs
When internal observations point directly to mechanical, electrical, or structural failures—such as burner flame failures, faulty variable frequency drives, or air-volume imbalances—escalate the issue to certified personnel.
Providing a structured fault packet eliminates guesswork and helps reduce paint booth downtime:
QUALIFIED SERVICE HANDOFF
- ☐ Digital images of control panels and active alarm codes
- ☐ High/low differential manometer readings under full fan load
- ☐ Filter maintenance dates, styles, and part numbers
- ☐ Air compressor dew point and desiccant maintenance logs
- ☐ Specific coating lines, substrates, and mix ratios involved
- Digital photos of displays and hardware: Capture clear images of active fault screens, error code sub-menus, and mechanical differential gauges running under full fan load. Photograph any media track warping or damper linkage issues.
- Current operating and maintenance logs: Include the date of the last filter rotation, the brand and media class installed, and recent preventative maintenance on the air make-up burner or shop compressors.
- Environmental baseline: Note ambient facility conditions, including exterior weather shifts, shop humidity levels, and heating plant transitions.
- Controlled post-repair verification: Have qualified personnel confirm the authorized return-to-service checks and record whether the original symptom recurs under comparable approved conditions before production release.
Source Matching Replacement Components
Cabin maintenance requires reliable, properly matched replacement components that meet factory specifications. If your triage reveals degraded door gaskets, damaged latches, failing light fixtures, or saturated intake and exhaust filters, install components built specifically for your cabin’s airflow profile.
To identify correct replacement components, exhaust arrestors, or ceiling diffusion media for your setup, Request a Quote with your booth manufacturer name, model number, internal cabin dimensions, and component serial tags.